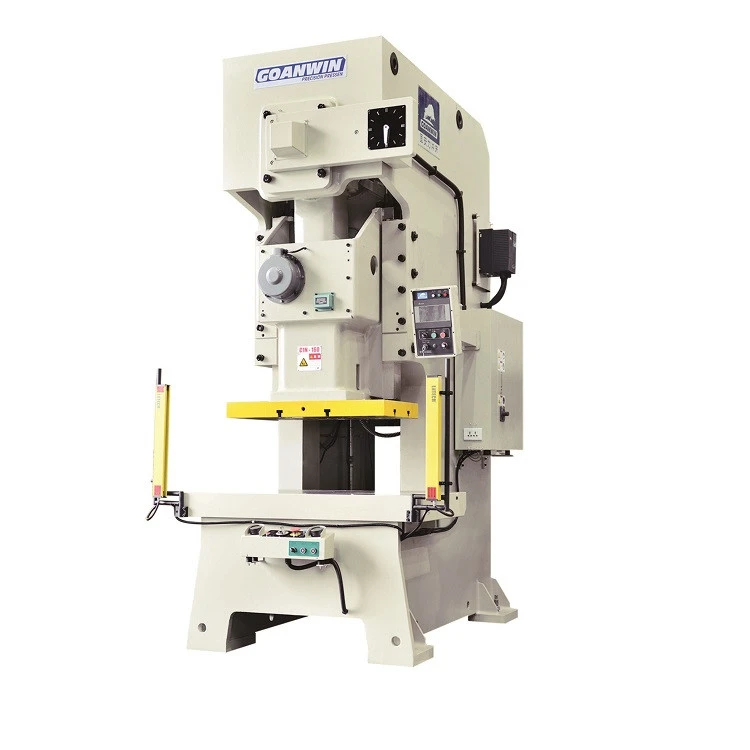
Single Crank Presses in This Range
A single crank press drives its slide from one crank and one connecting point. In this manufacturer's range the layout appears in four published series: two gap frame series — the C1N (15-400 tons) and the A1 (25-315 tons) — and two straight side series — the D1N (80-260 tons) and the M1N (125-800 tons). The same single-crank layout is also listed in the manufacturer's platform catalogue for straight side models, so the configuration spans the catalogue from the smallest bench-scale blanking work to 800-ton straight side production.
| Series | Frame | Capacity | Stroke | SPM |
|---|---|---|---|---|
| C1N | C-frame (gap frame) single crank | 15-400 t | 30-300 mm | 20-200 |
| A1 | C-frame (gap frame) single crank | 25-315 t | 30-250 mm | 20-190 |
| D1N | Straight side single crank | 80-260 t | 70-250 mm | 20-120 |
| M1N | Straight side single crank | 125-800 t | 80-300 mm | 10-90* |
Ranges above are the span of each series' published Technical Datas table. Selected per-model specifications — die height, bolster and slide dimensions, cushion capacity, motor and weight per model — are published on the C-frame press page (C1N, A1) and the H-frame press page (D1N, M1N). (Source note on the range marked * in the table: the M1N speed range opens at 10 because the M1N-800's variable SPM cell is printed in the manufacturer's table as a date, “10月20日”; the 10 is a presumed restoration of that value — treat it as presumed, not as a resolved specification, and have it confirmed by the manufacturer when quoting.)
What One Crank Point Means at the Die
With a single connecting point, the slide is driven at its centre; the two-point series in the same catalogue apply the drive at two points along the slide instead. The manufacturer's own pages document the single crank series for this work: the A1 page documents blanking, punching, bending and forming on small single work of thin steel plate and progressive die parts, and the C1N page documents stamping small parts at high single-stroking rates or in continuous mode, using either blanks or coil stock. The A1 page documents its two frame variants (V and H) with different standard SPM and stroke combinations, and the C1N table does the same for its larger models: the target output is one of the details to state with the enquiry.
Documented Features of the Single Crank Series
- Precision grade: the published tables state GB (JIS) Class 1 precision for the C1N, D1N and M1N series; the A1 table carries no precision-grade row.
- Overload protection: a fast-response hydraulic overload protection system is a published standard feature on the C1N, D1N and M1N pages — it relieves an overload, stops the press immediately and protects press and dies.
- Clutch, brake and lubrication: a high-torque, low-noise clutch and brake unit and a forced lubrication system with monitoring are documented across the mechanical range.
- Die cushions: pneumatic die cushions are published across the single crank series — for example 2.3 to 14 tons on the C1N table and, on the A1, a cushion from the A1-45 model upward.
- Automation connection: the C1N page documents connection with single presses, progressive dies, mechanical arms and transfer systems.
The same catalogue also lists two-point machines, on the double crank press page. The full mechanical range, including the servo and eccentric alternatives, is indexed on the mechanical presses page.
Frequently Asked Questions
What is the smallest and largest single crank press here?
The C1N starts the range at 15 tons; the M1N straight side single crank series tops it at 800 tons. Per-model figures are tabled on the C-frame and H-frame family pages.
Single crank or double crank for a progressive die?
The two-point series (C2N, D2N, T2N) are the documented layout for long dies with stations spread across the bolster, on the double crank page; which layout a given die is quoted on is settled in the enquiry against its width and load spread.
Are single crank presses available with a die cushion?
Yes — pneumatic die cushions are published across the series, for example 2.3 to 14 tons on the C1N and from the A1-45 upward on the A1. Cushion force and stroke per model are in the family-page tables.
Can SPM or stroke be changed from the table values?
The manufacturer's product pages state that presses can be customized for a wider range of SPM, stroke, rating point (BDC), bed and other dimensions; the changed figures are fixed in the written quotation.
Send an Enquiry
Tell us the machine, your material and thickness, and the part you are forming. Tonnage, configuration and price are confirmed in the written quotation.